

Manufacture of cast iron components: From raw material to finished component
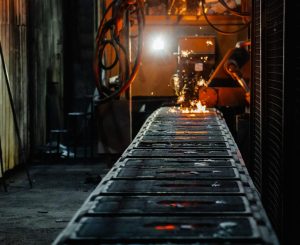
The Schlumberger Foundry produces cast iron components weighing between 0.1 and 600 kg, in small and medium-sized batches ranging from 5 to 10,000 pieces per year, at its site in Guebwiller, Alsace. From co-design to dispatch, the entire process can be coordinated in-house through a single point of contact, ensuring seamless traceability.
The scope of work – whether raw or finished parts – is defined with you in advance, before any production begins.
Foundry process, sand casting using green sand
Design & simulation
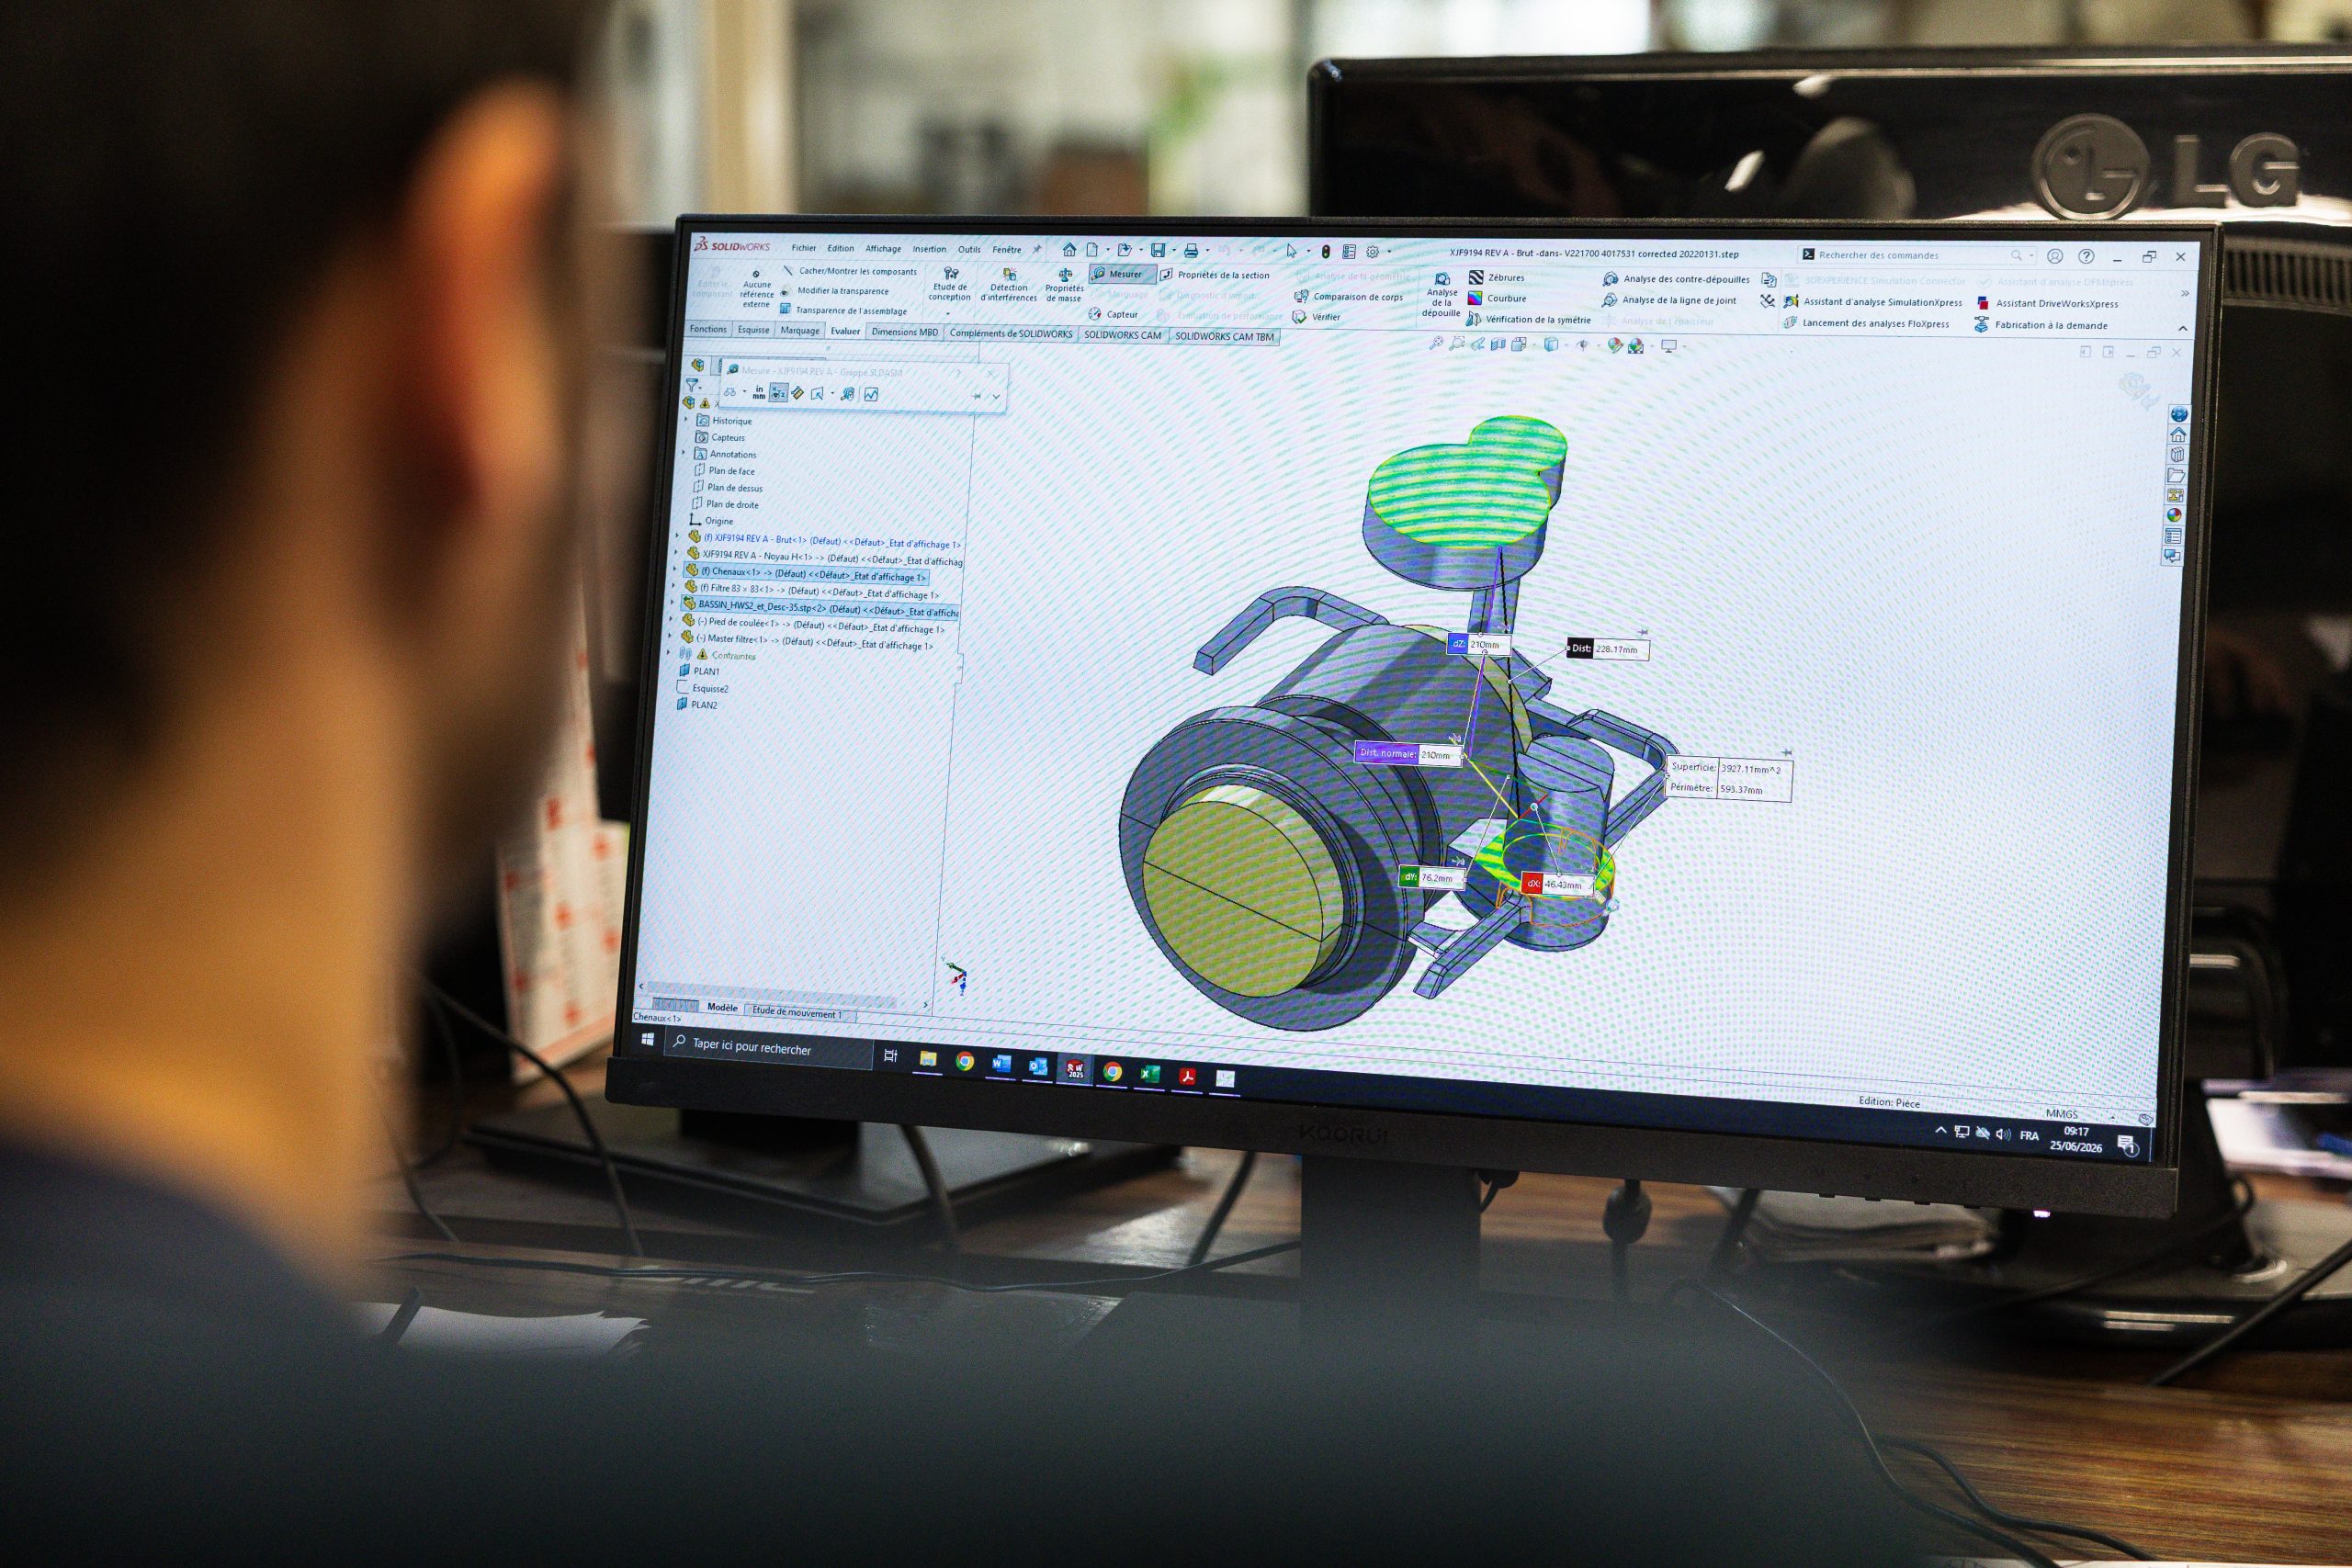
The design/planning as well as and the management of the manufacture of tools, moulds, core boxes, core boxes, weights, is carried out entirely in-house.
- CAO : SolidWorks
- Casting simulation: Nova Flow, supporting the technical expertise of our production engineering department.
- Prototyping: 3D sand printing, without the need for specialised tooling
Core making
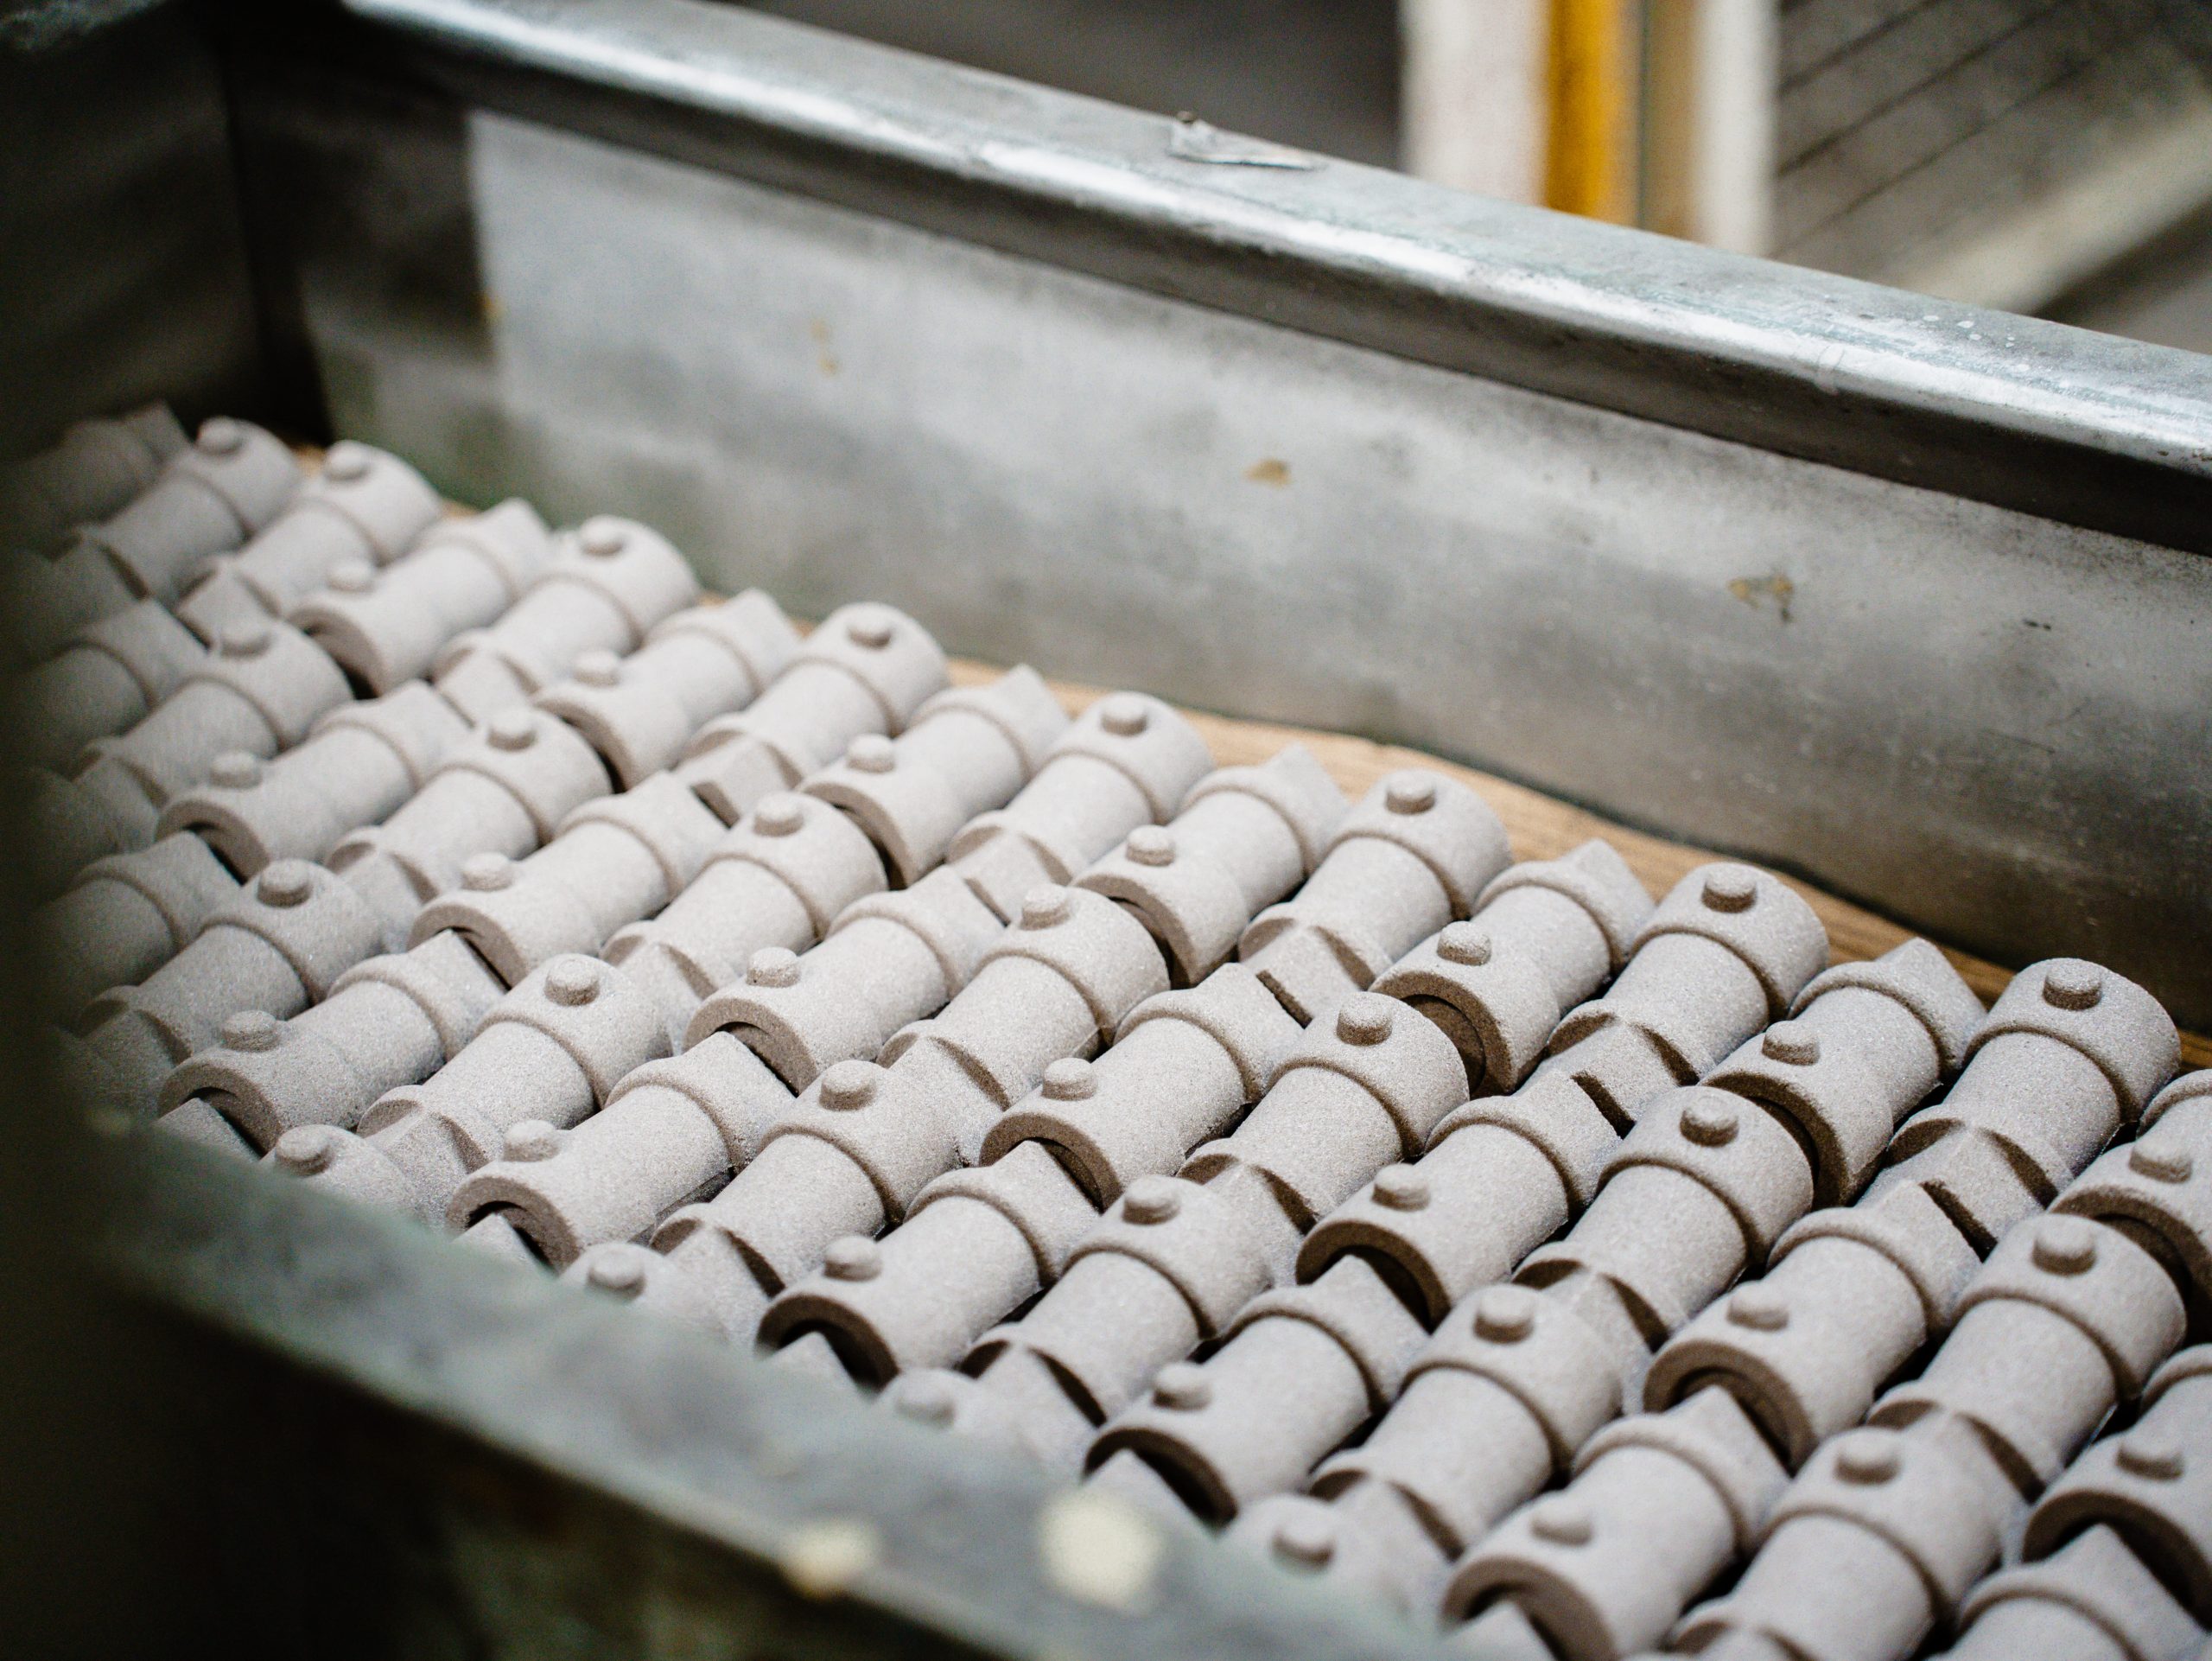
- 3 pitting automatic Laempe machines: 5, 20 and 40 litres
- 1 Alphaset manual machine for the cores of large size or complex geometry
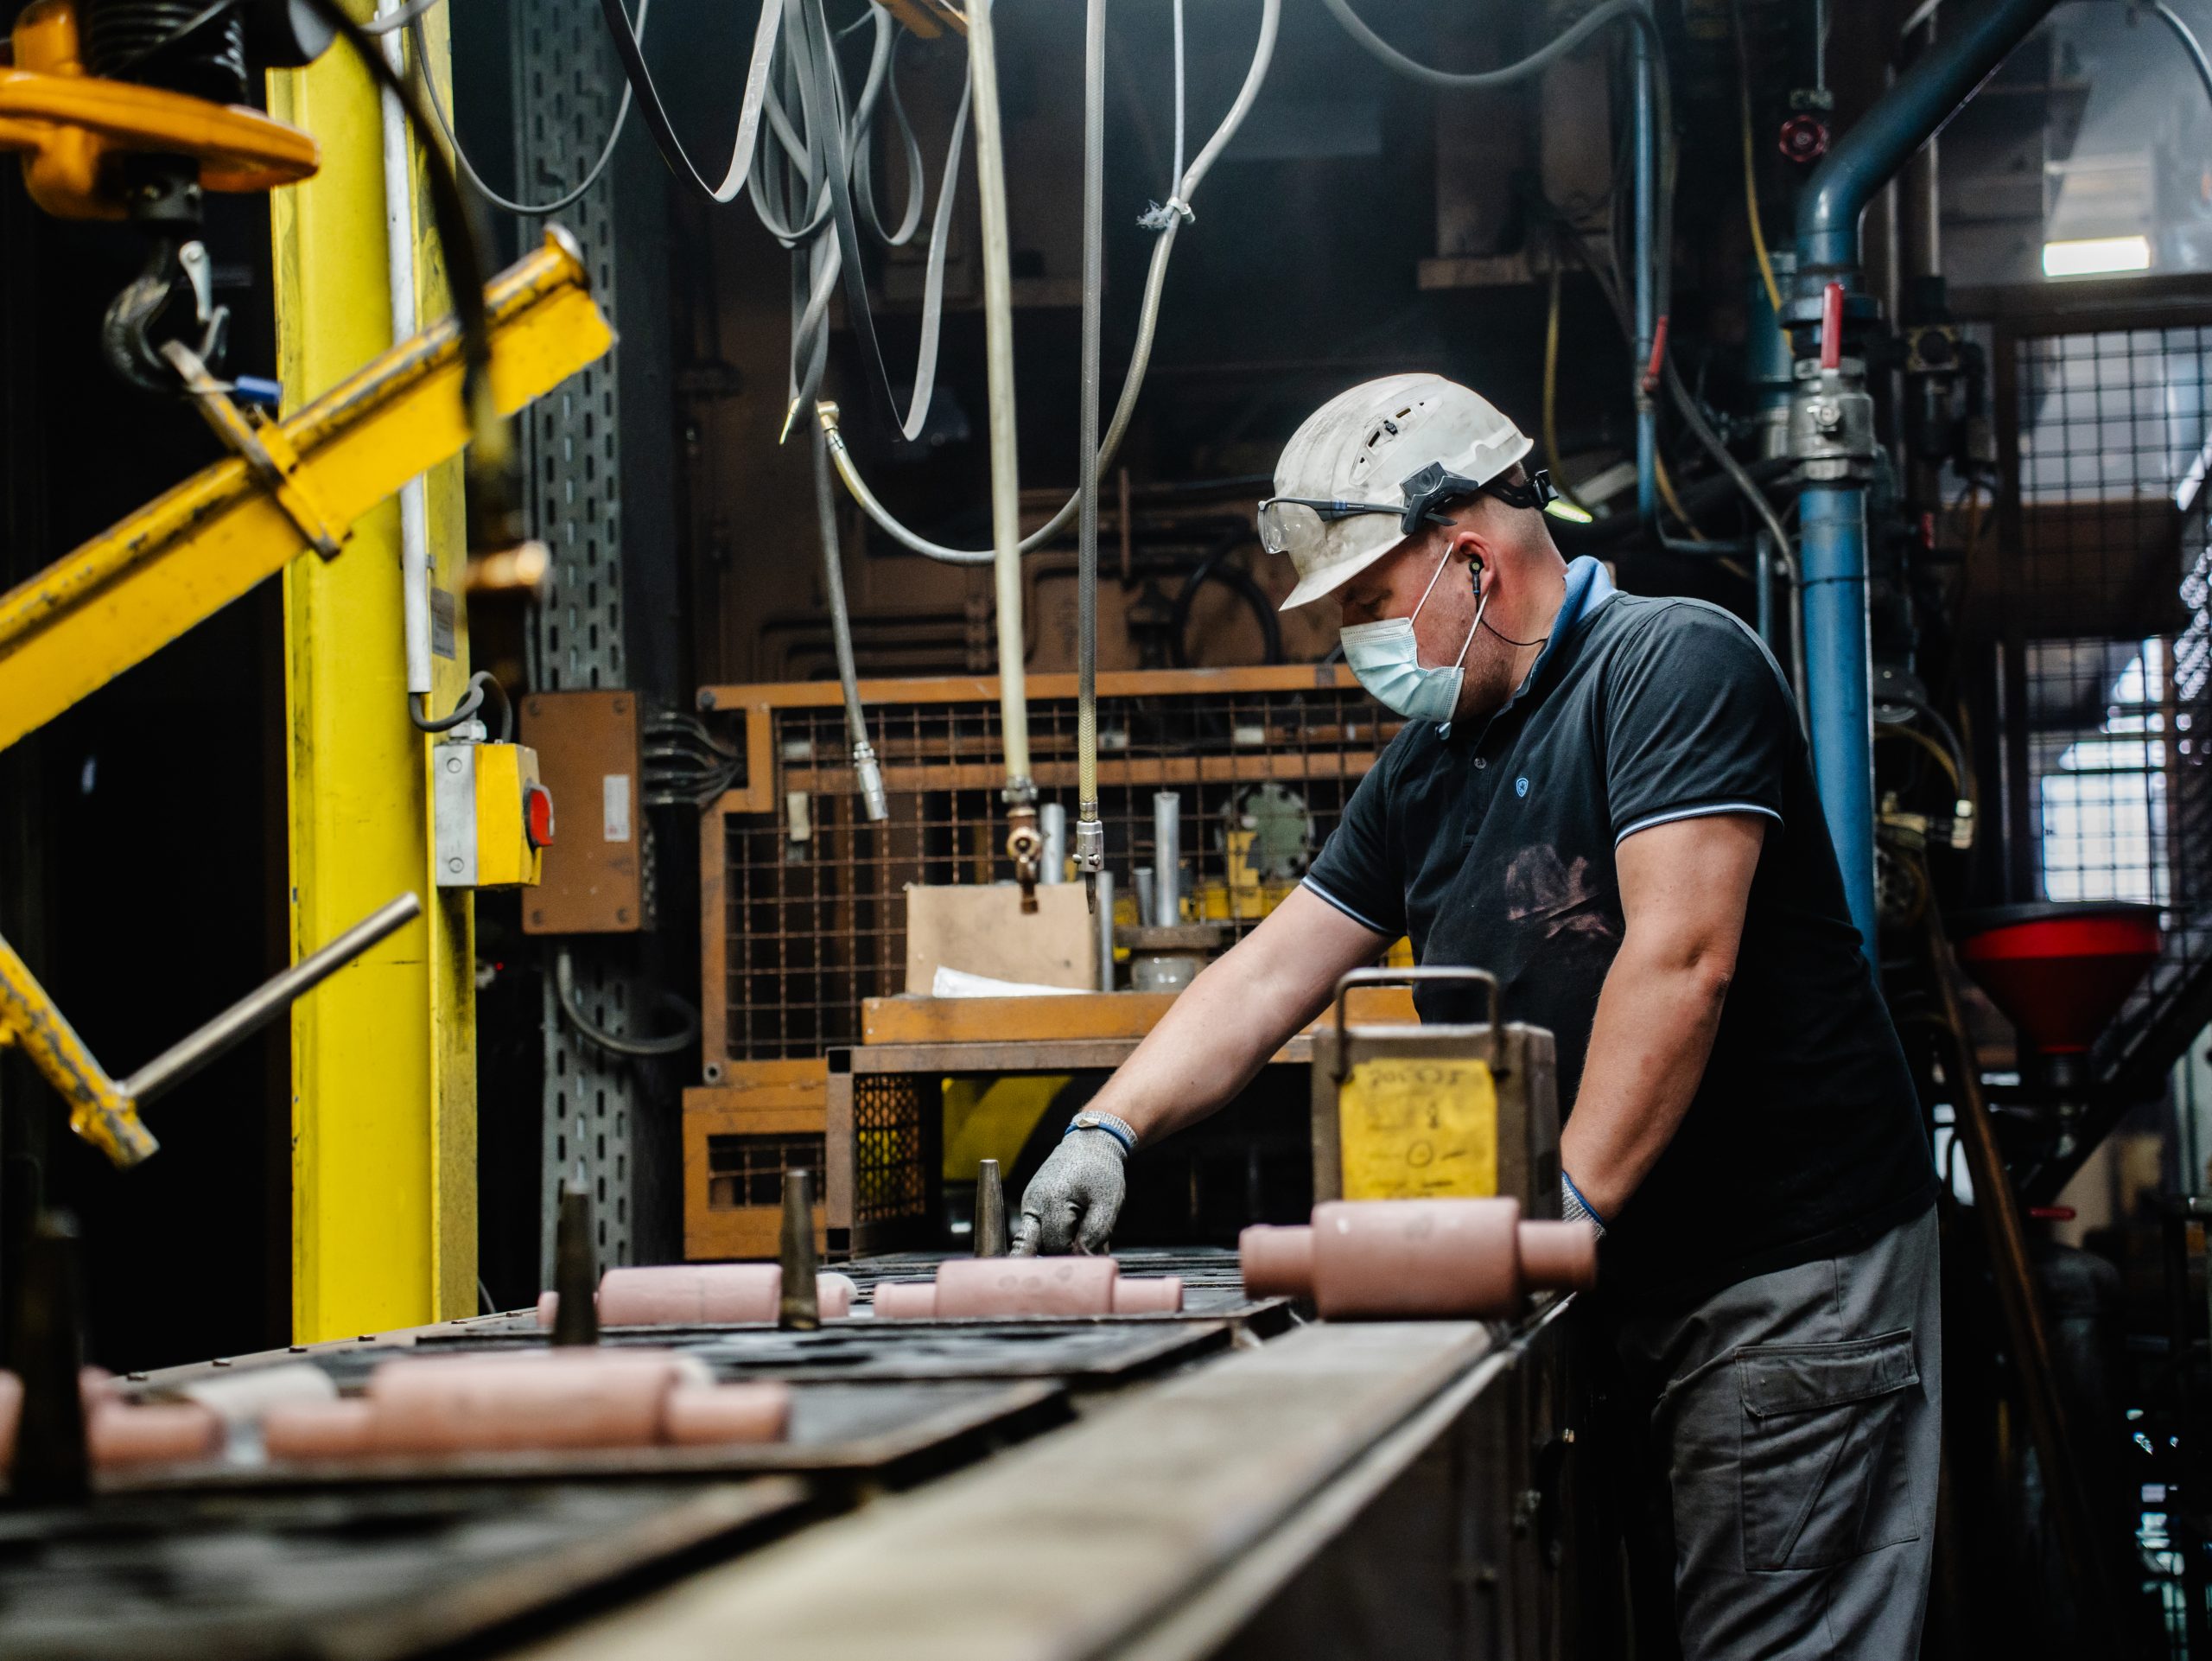
Molding of parts made of cast iron
- HWS 1: green sand, high-pressure moulding with a size of 1400×1500×700 mm, 15 moulds per hour
- HWS 2: green green, high-pressure compression moulding with a size of 560×560×400 mm, 100 moulds per hour
- Sandblasting plant automated Rotocontrol
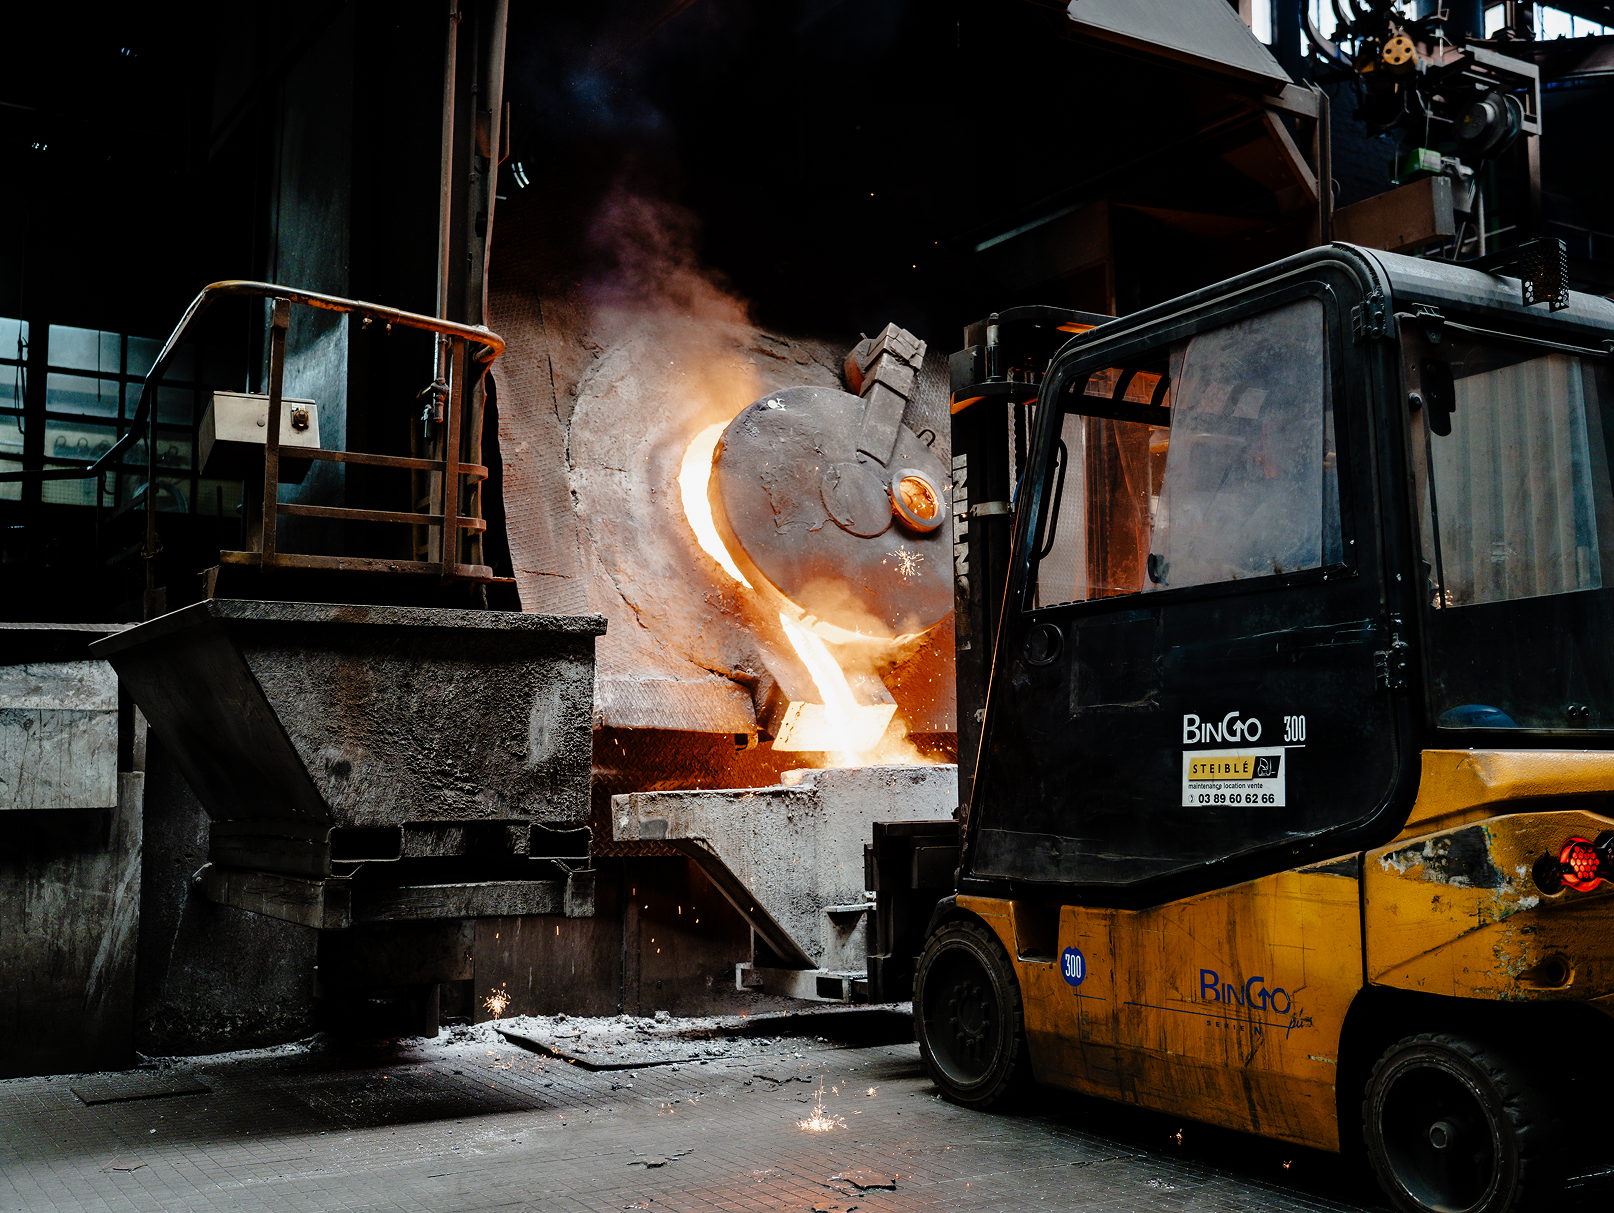
Melting
Cast iron GL, GS and ADI, three grades optimised for parts weighing up to 600 kg.
- 3 induction furnaces 4 tonnes, 1 furnace 5 tonnes
- Wire filled for the treatment of cast iron EN-GJS with spheroidal graphite
(link to the resources for the grades)
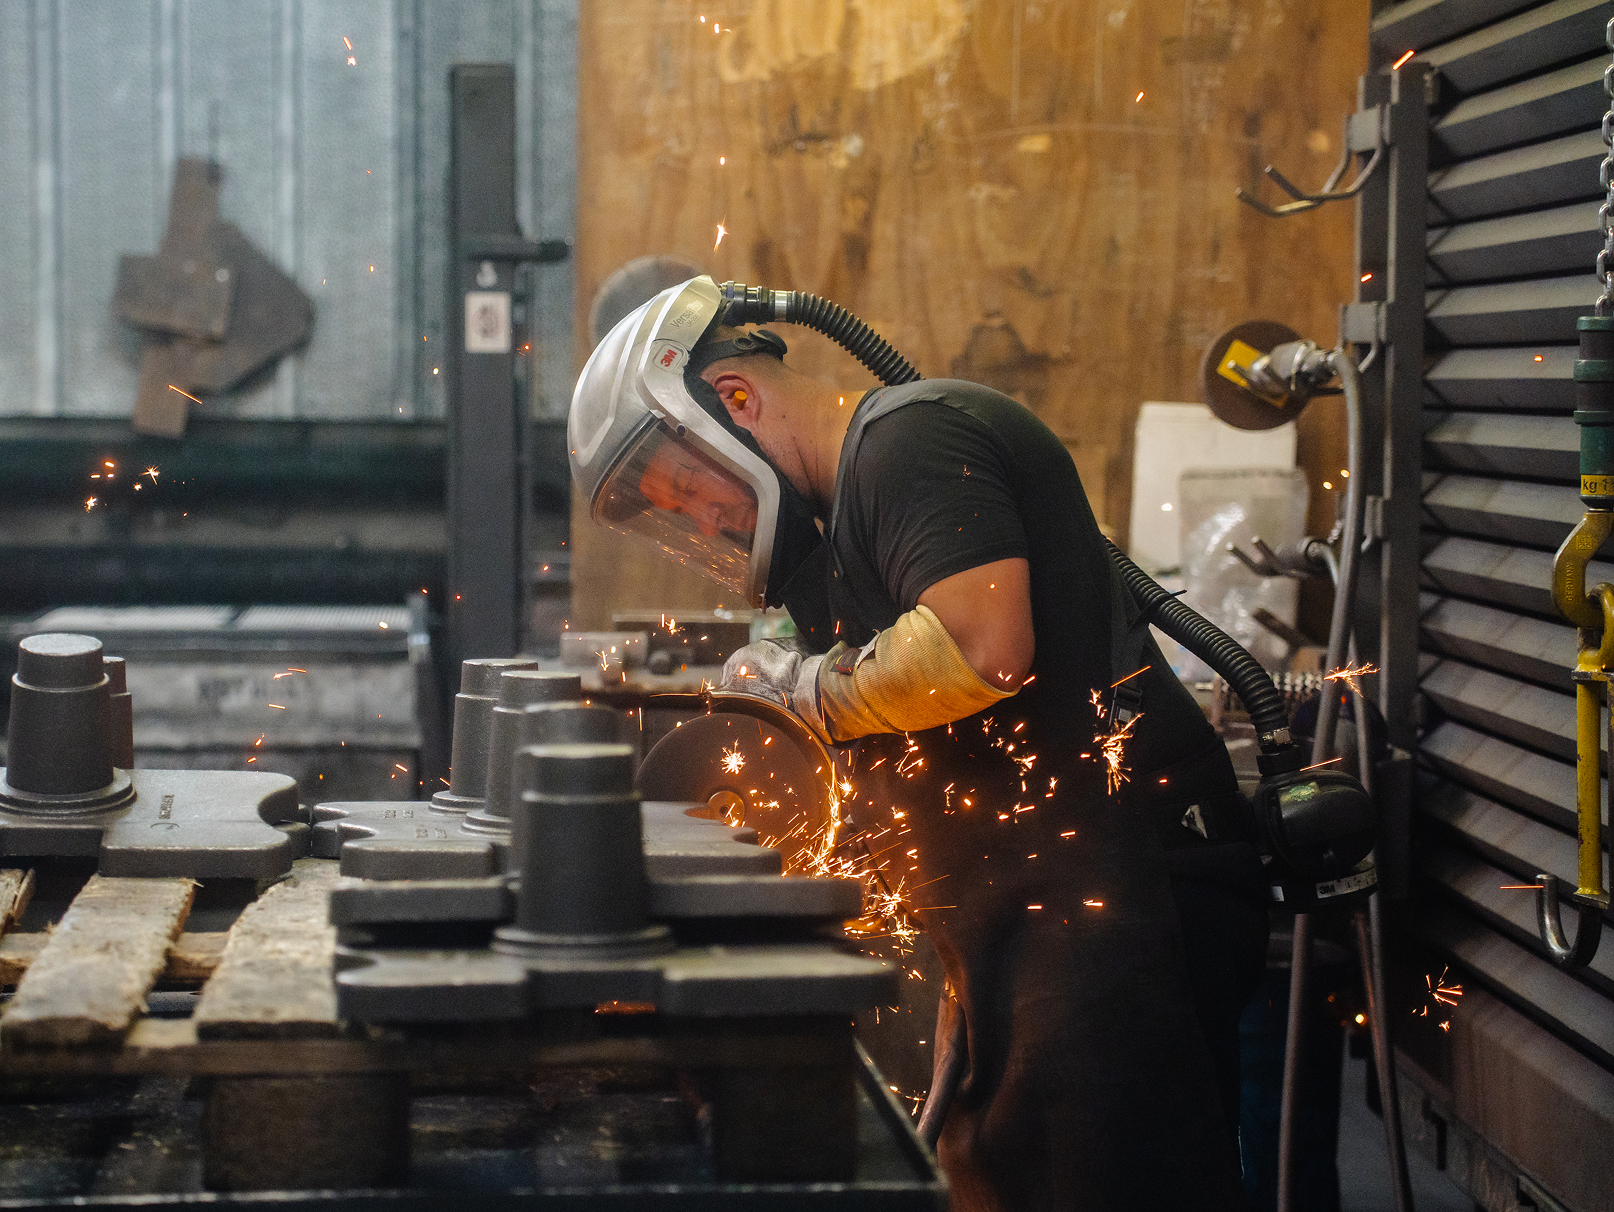
Finishing of cast iron parts
- Grenaillage : machine plateau Rump, machine tablier Wheelabrator.
- Deburring: grinding wheel, workbench, booth: seven workstations.
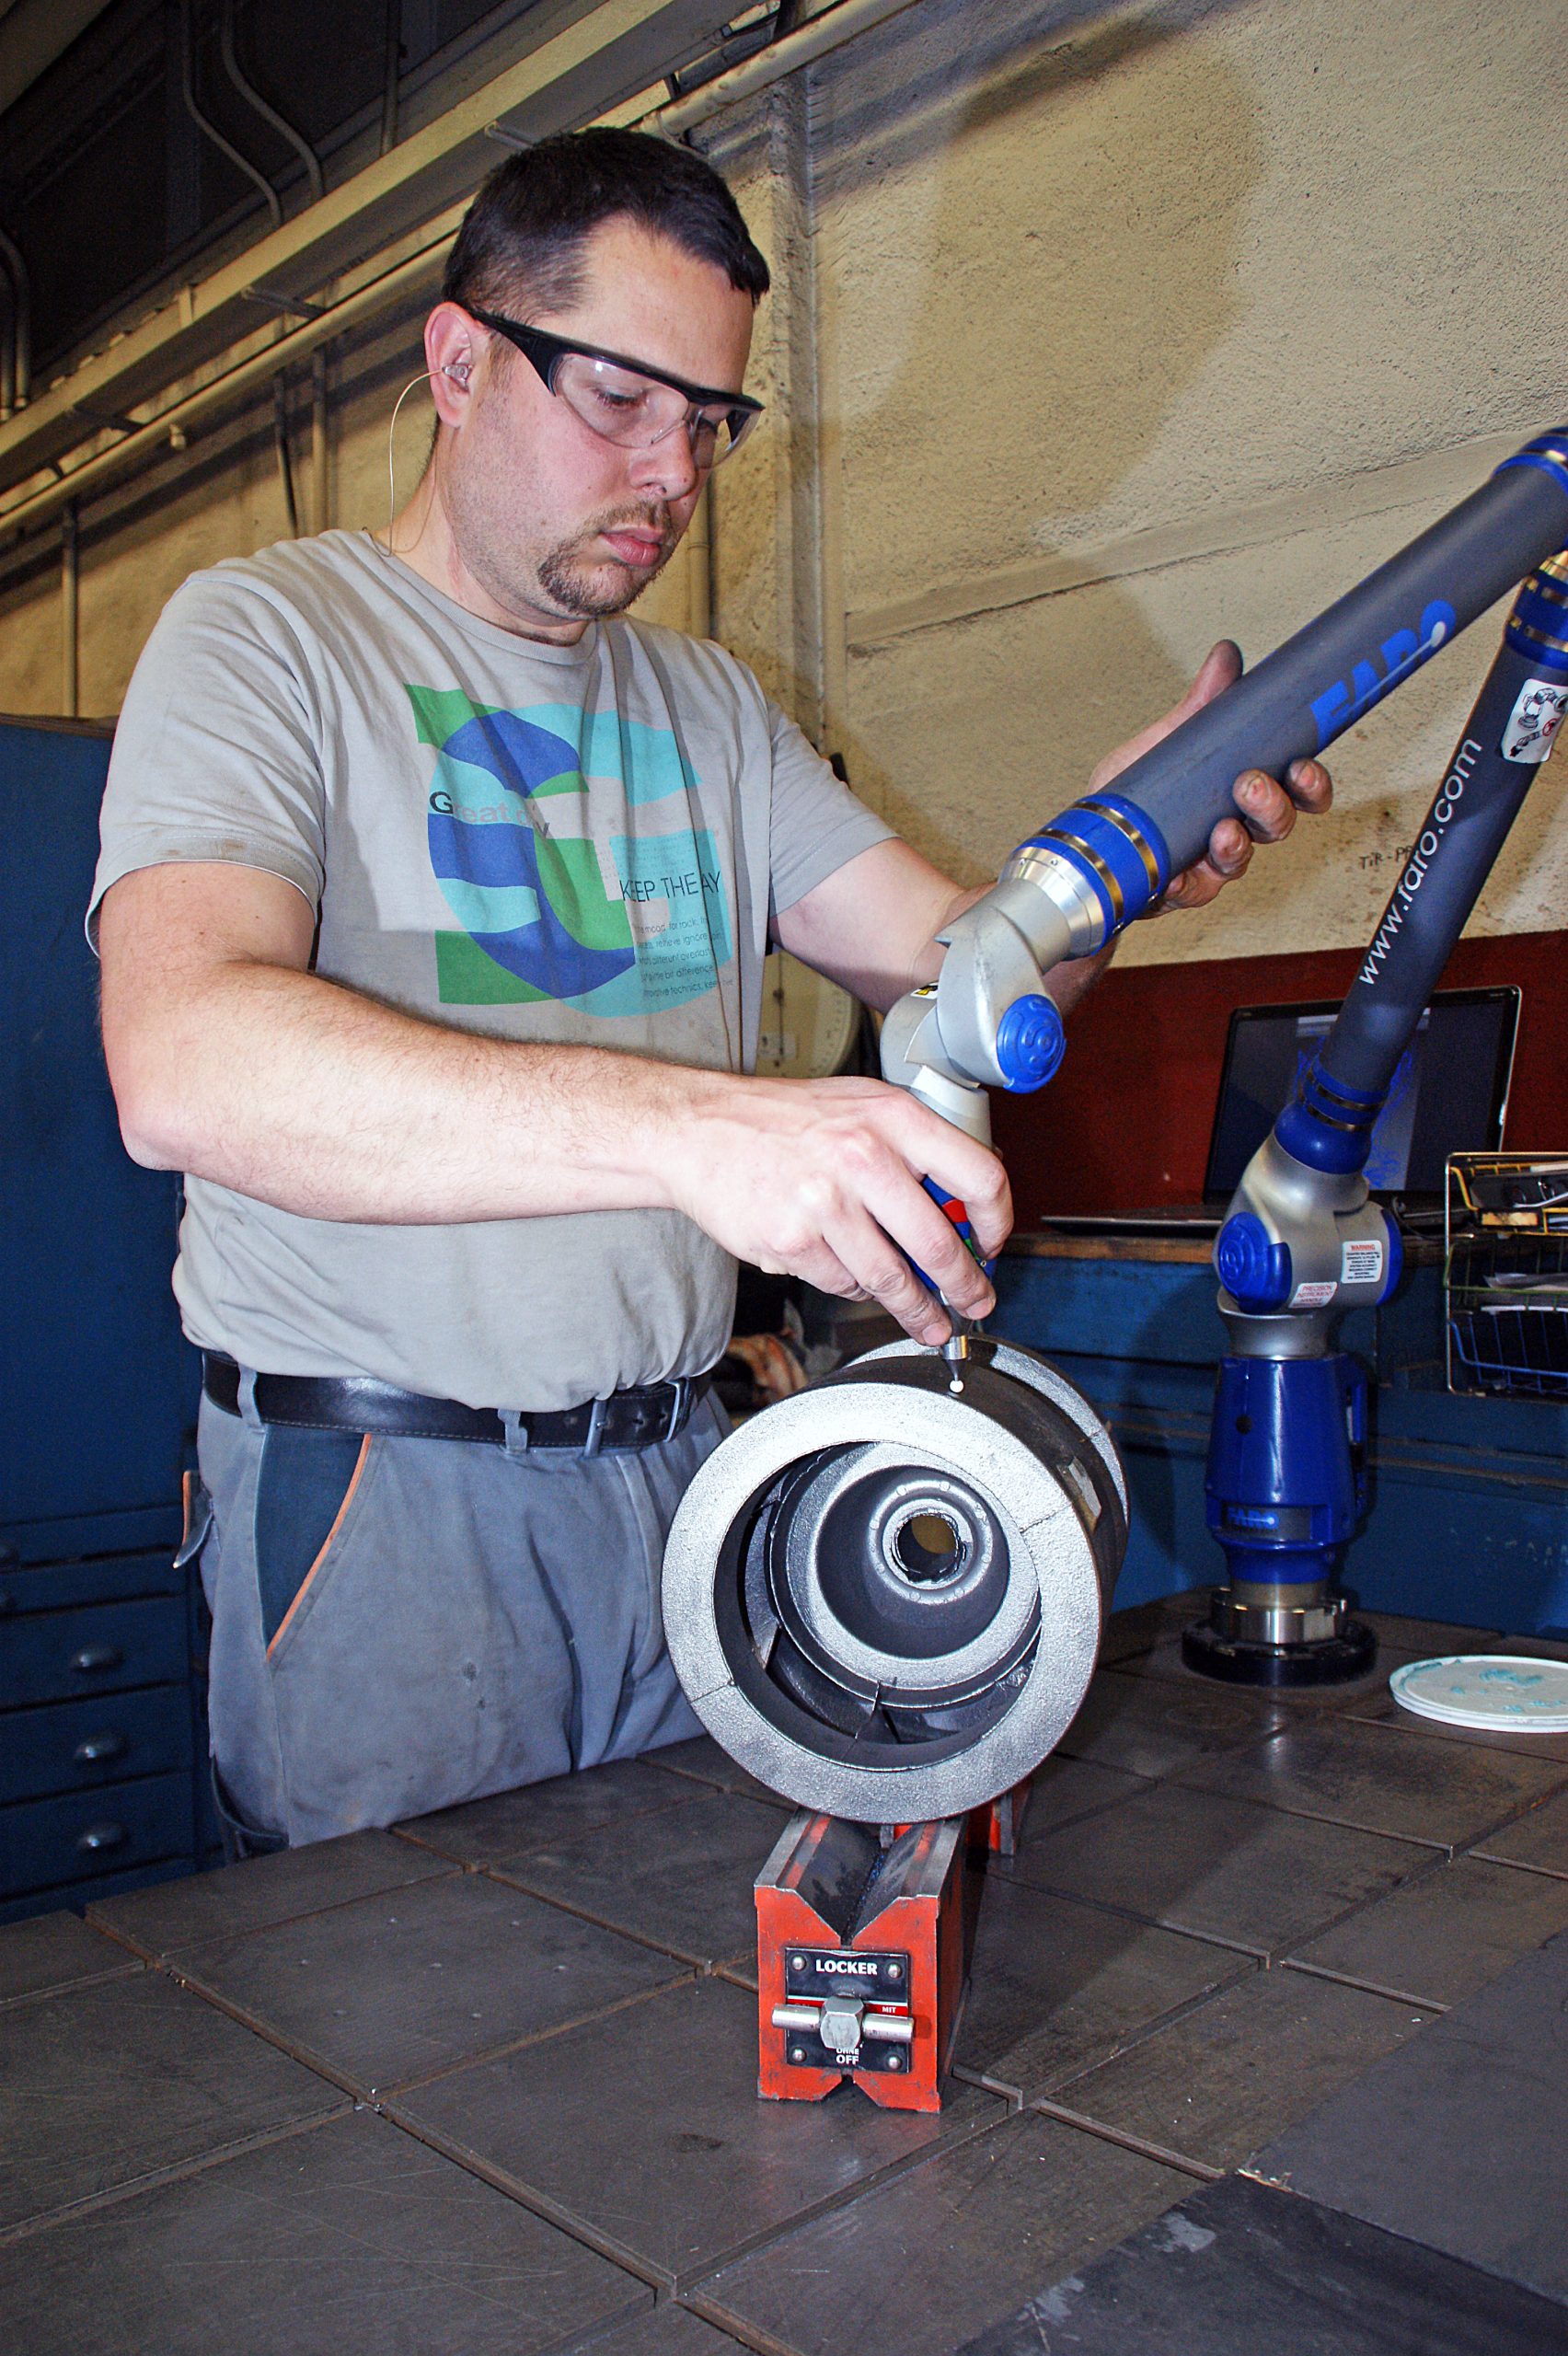
Quality control
Integrated into every stage, documented and traceable throughout the entire process.
- Material analysis: spectrometer, tensile testing machine, hardness testing, micrograph analysis, sand analysis
- Inspection of parts: conventional tools, Faro 3D measuring arms, ultrasound, penetrant testing
- Non-destructive inspections: radiography, magnetic particle testing
Operations supplementary
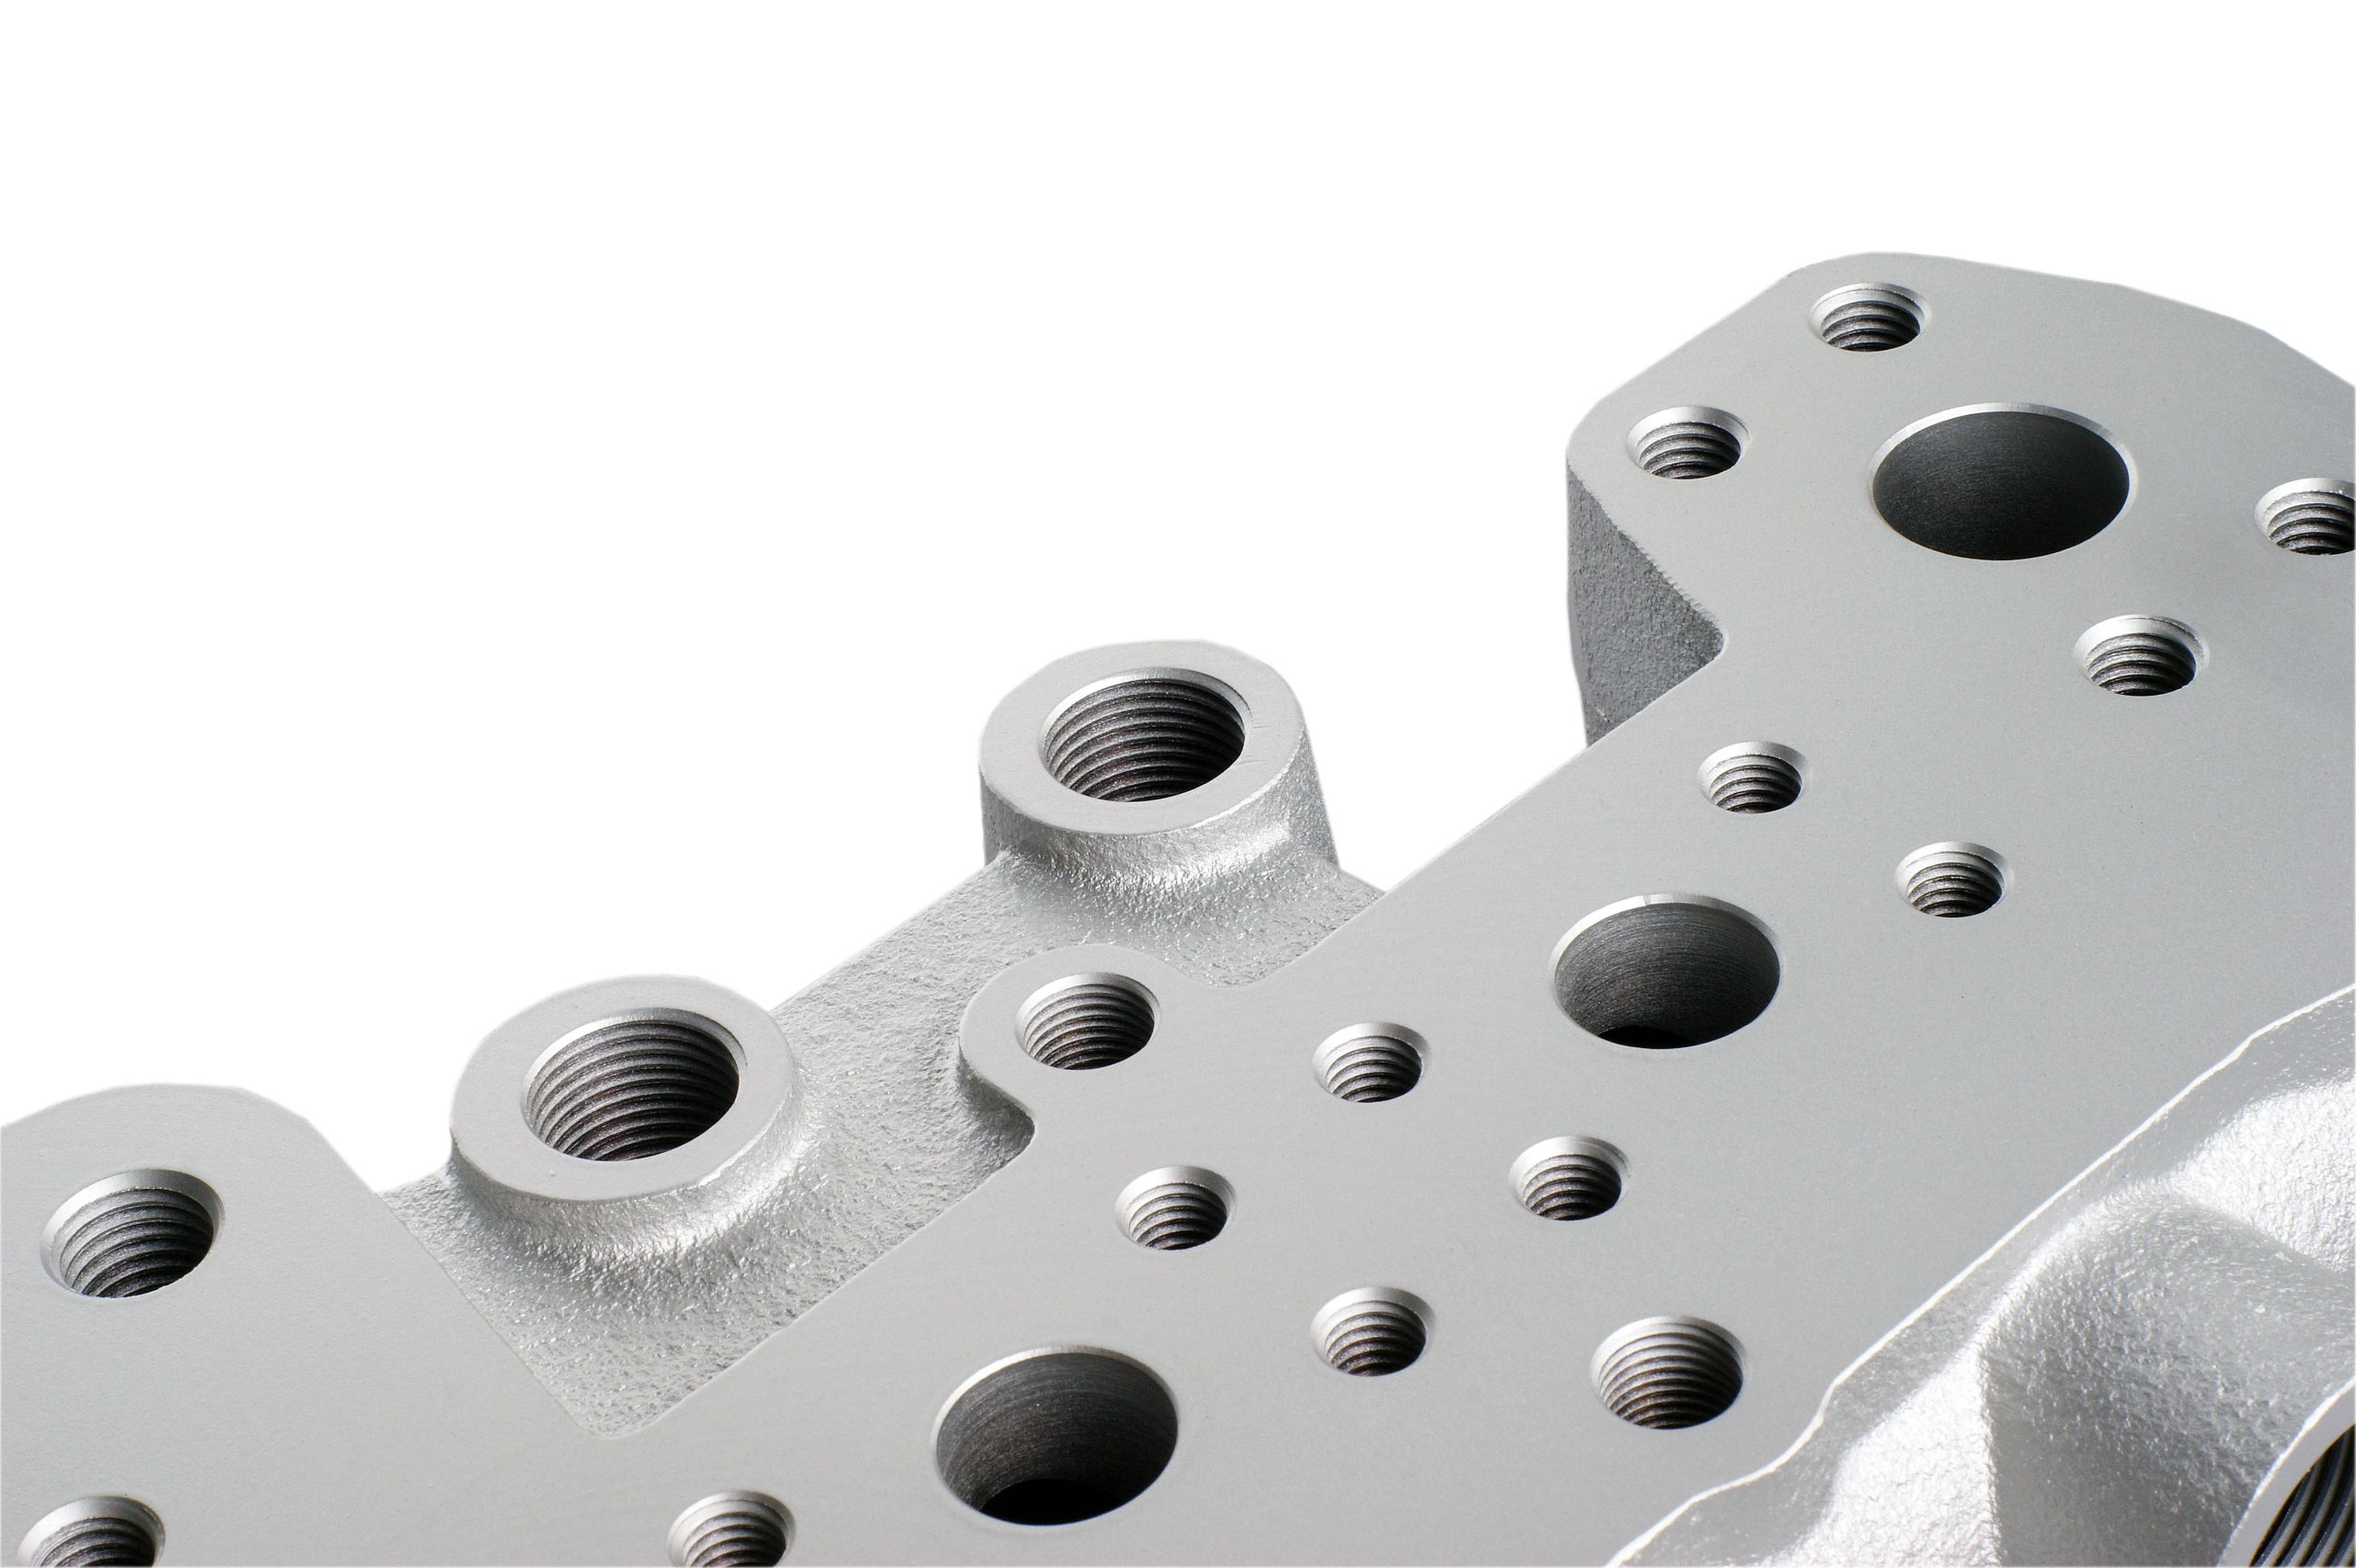
A network of selected partners in France, Belgium and Germany, chosen according to the technical and economic requirements of each project. The choice of partner is made either by the foundry or by the client.
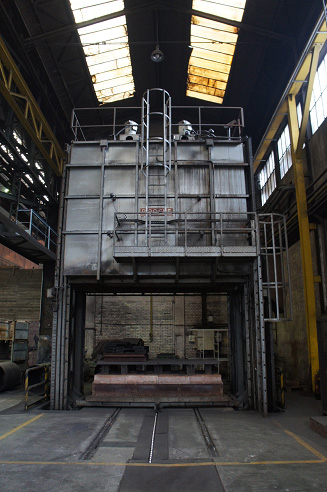
Stabilisation, ferritisation, annealing, treatment ADI: partners specialising in integrated solutions within the production process. Single point of contact.
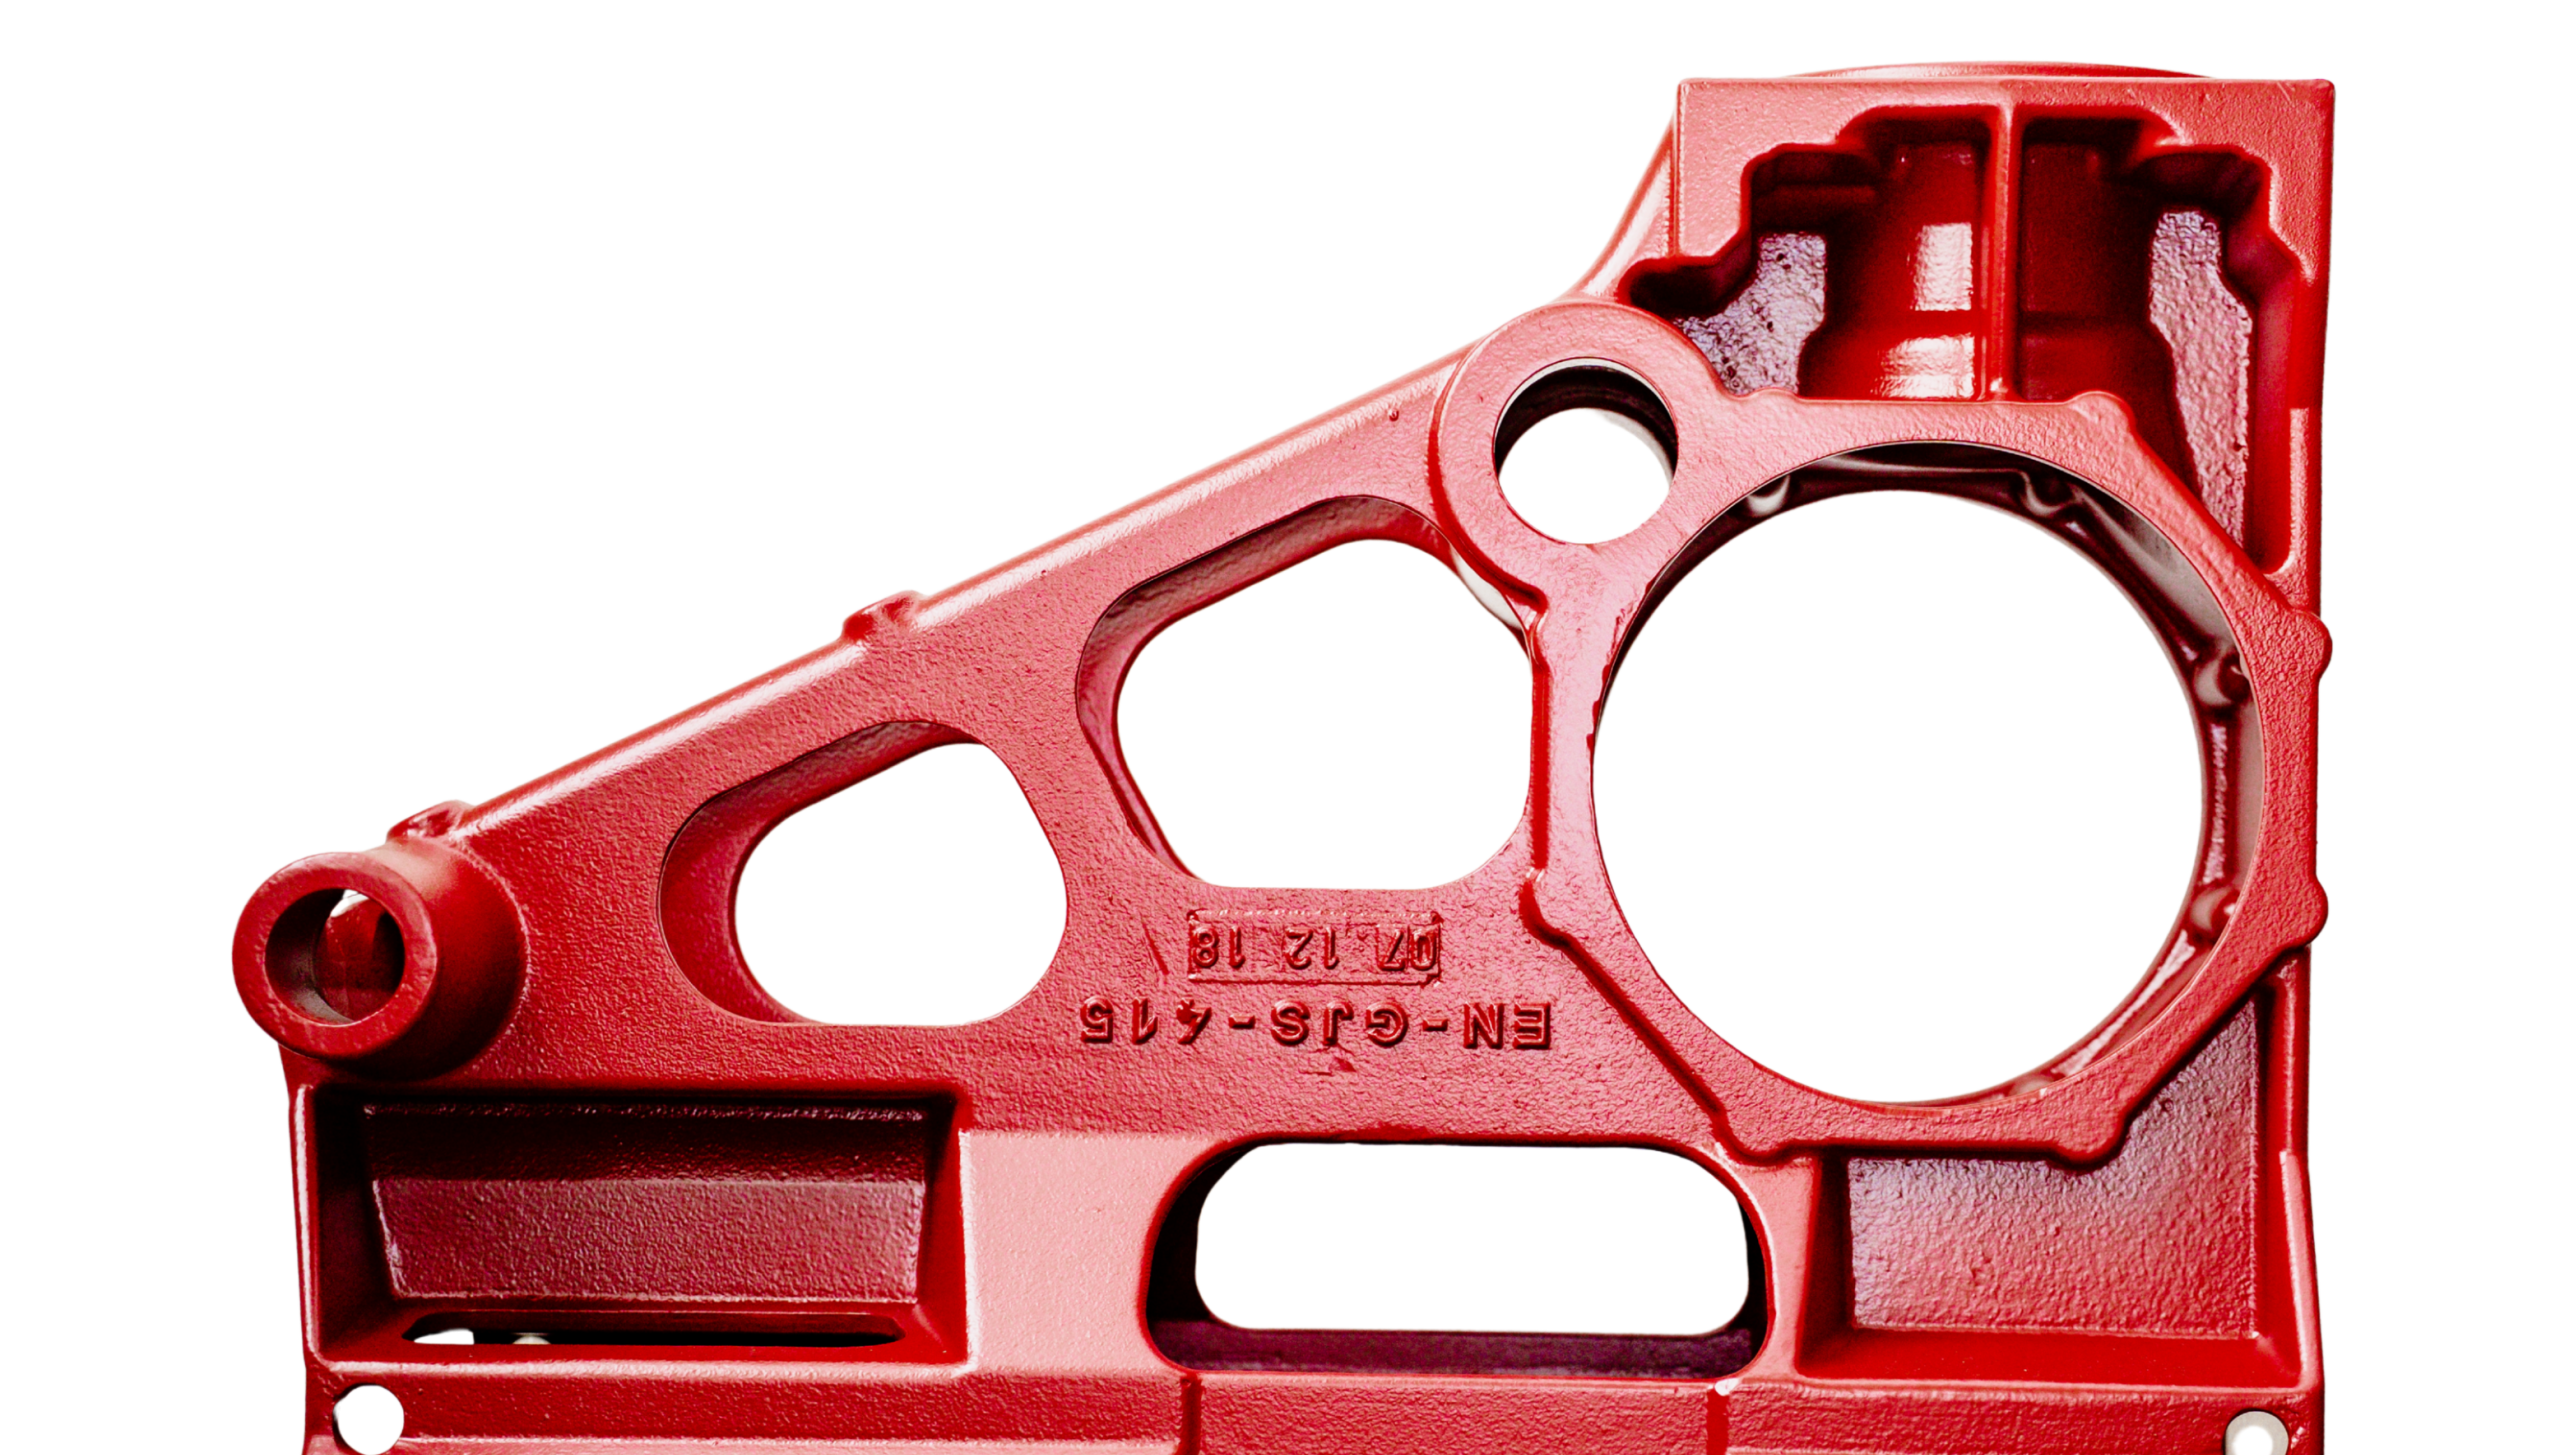
Dip coating or spray painting, cataphoresis, galvanising, bichromate coating. Same requirements, same traceability.
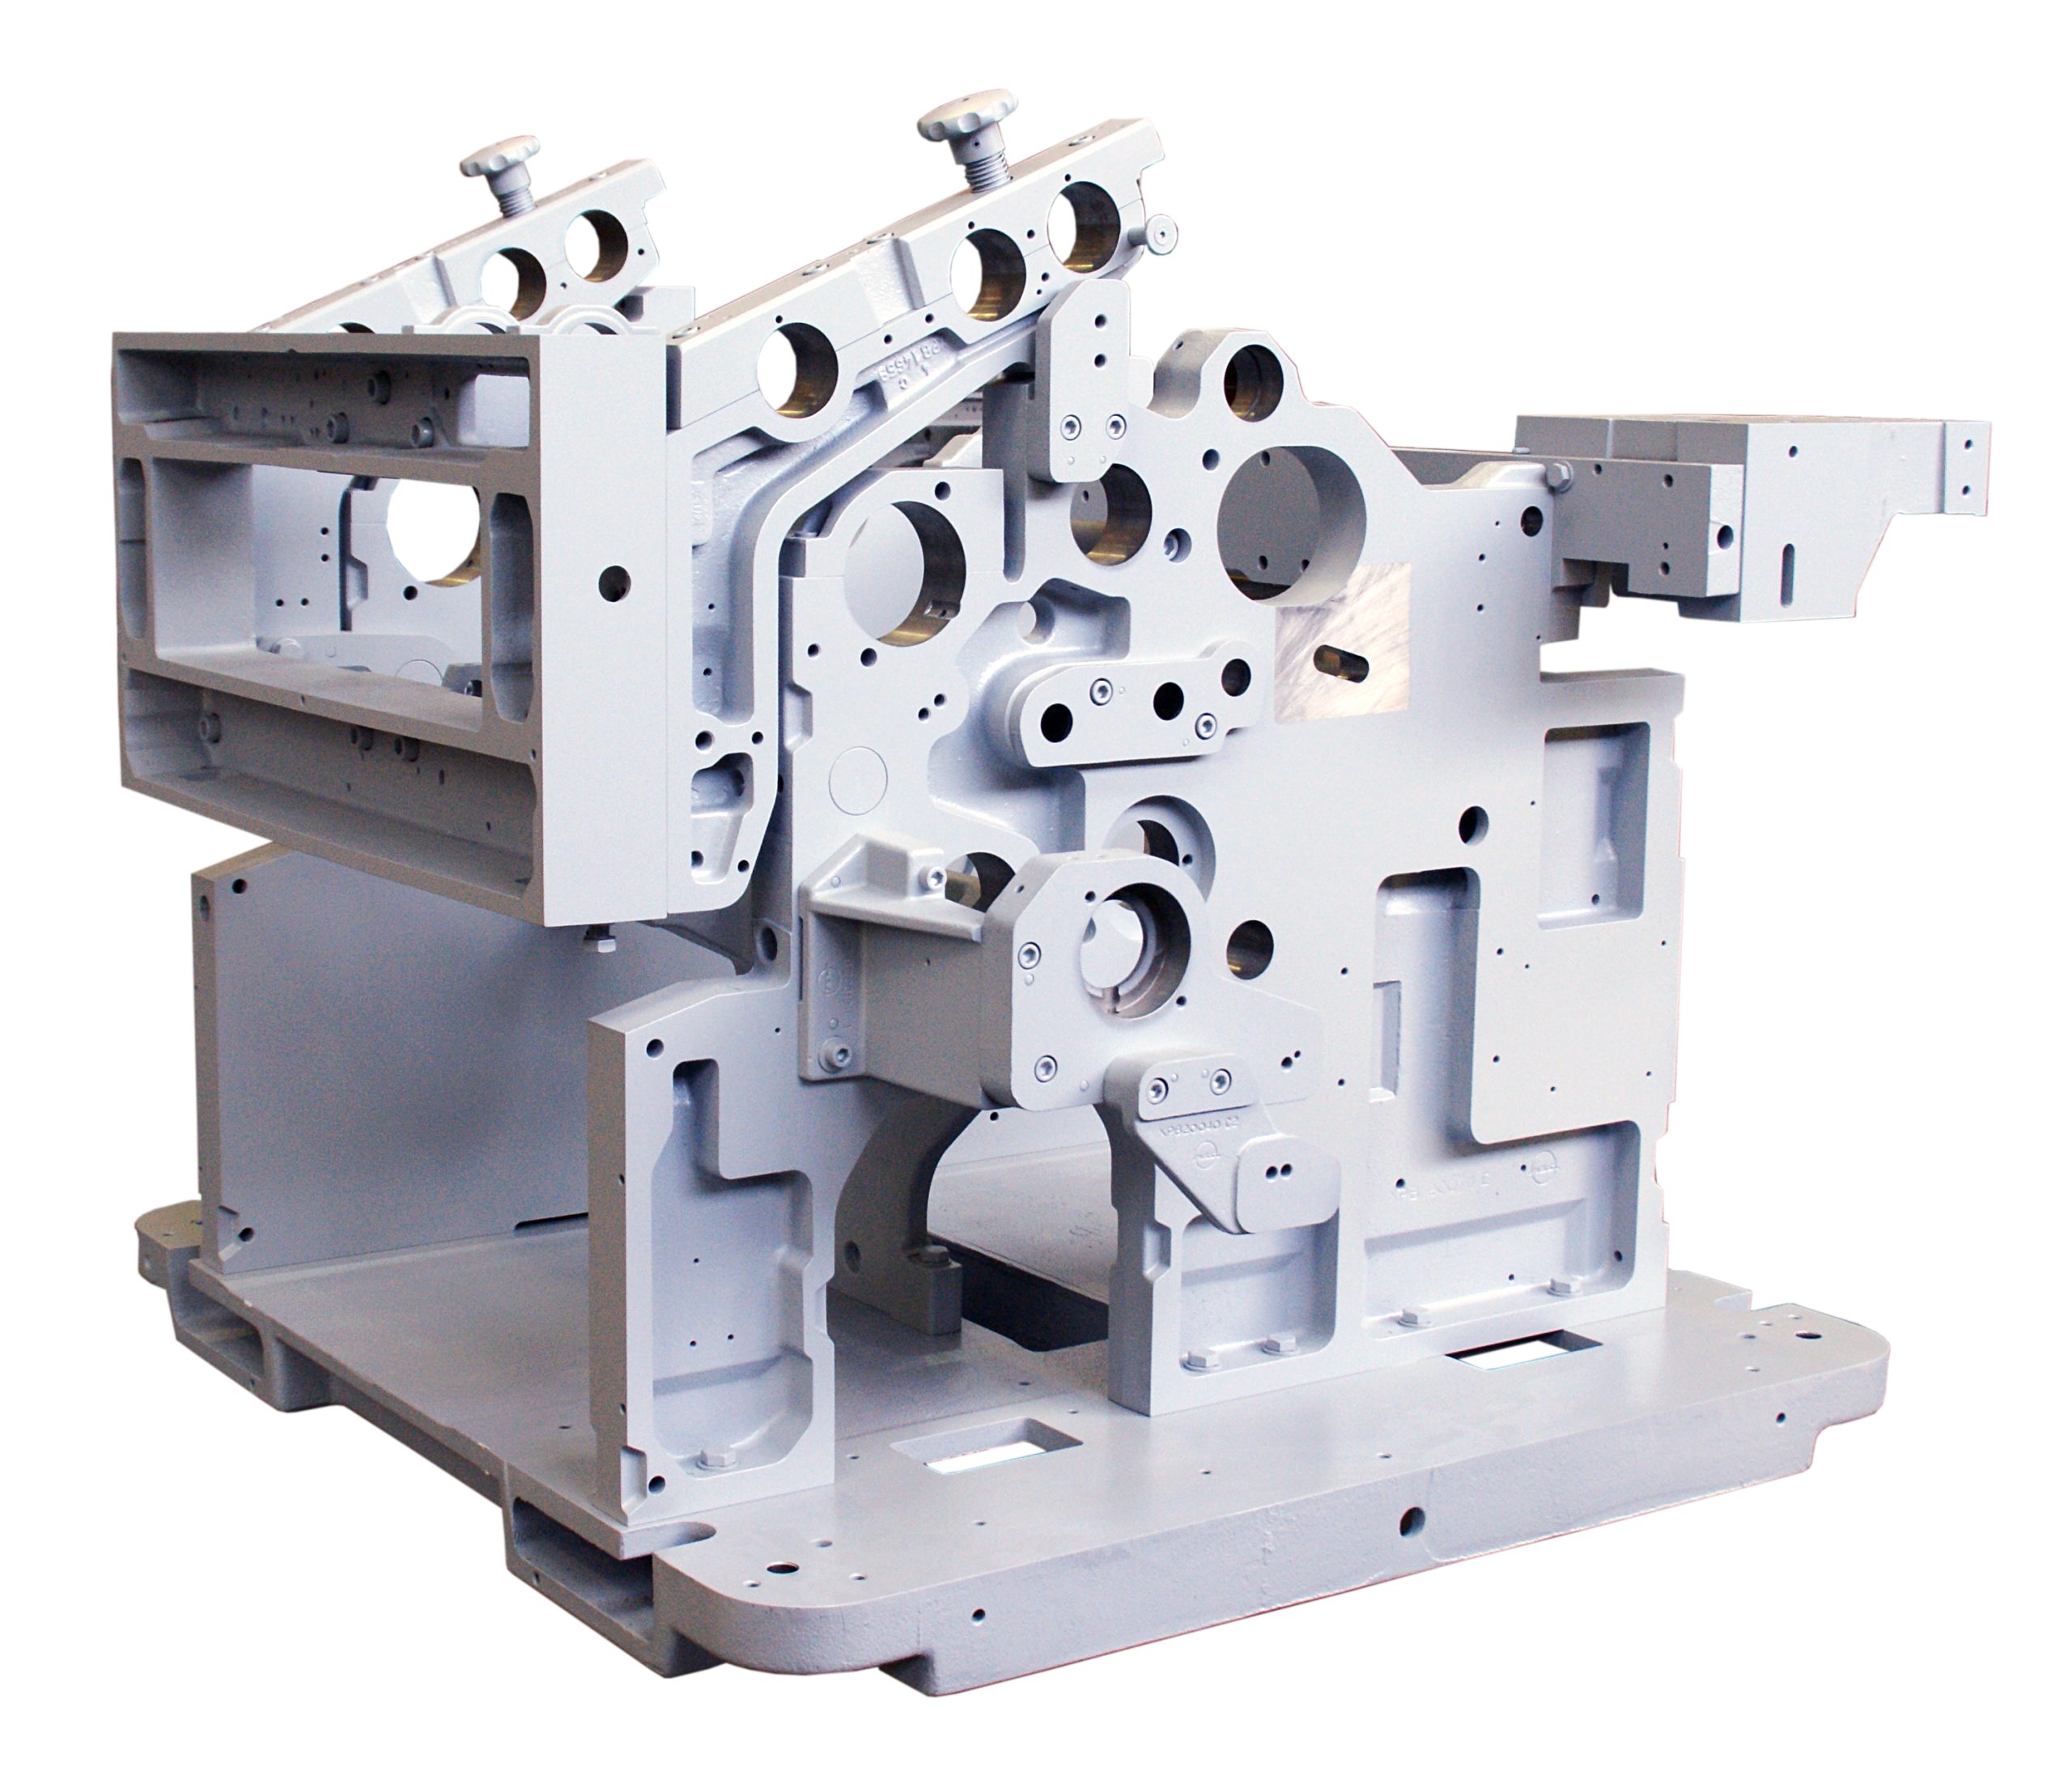
When the project requires it, we assemble the sub-assemblies before dispatch, fixings, add-on components, components and accessories. Final inspection before delivery.
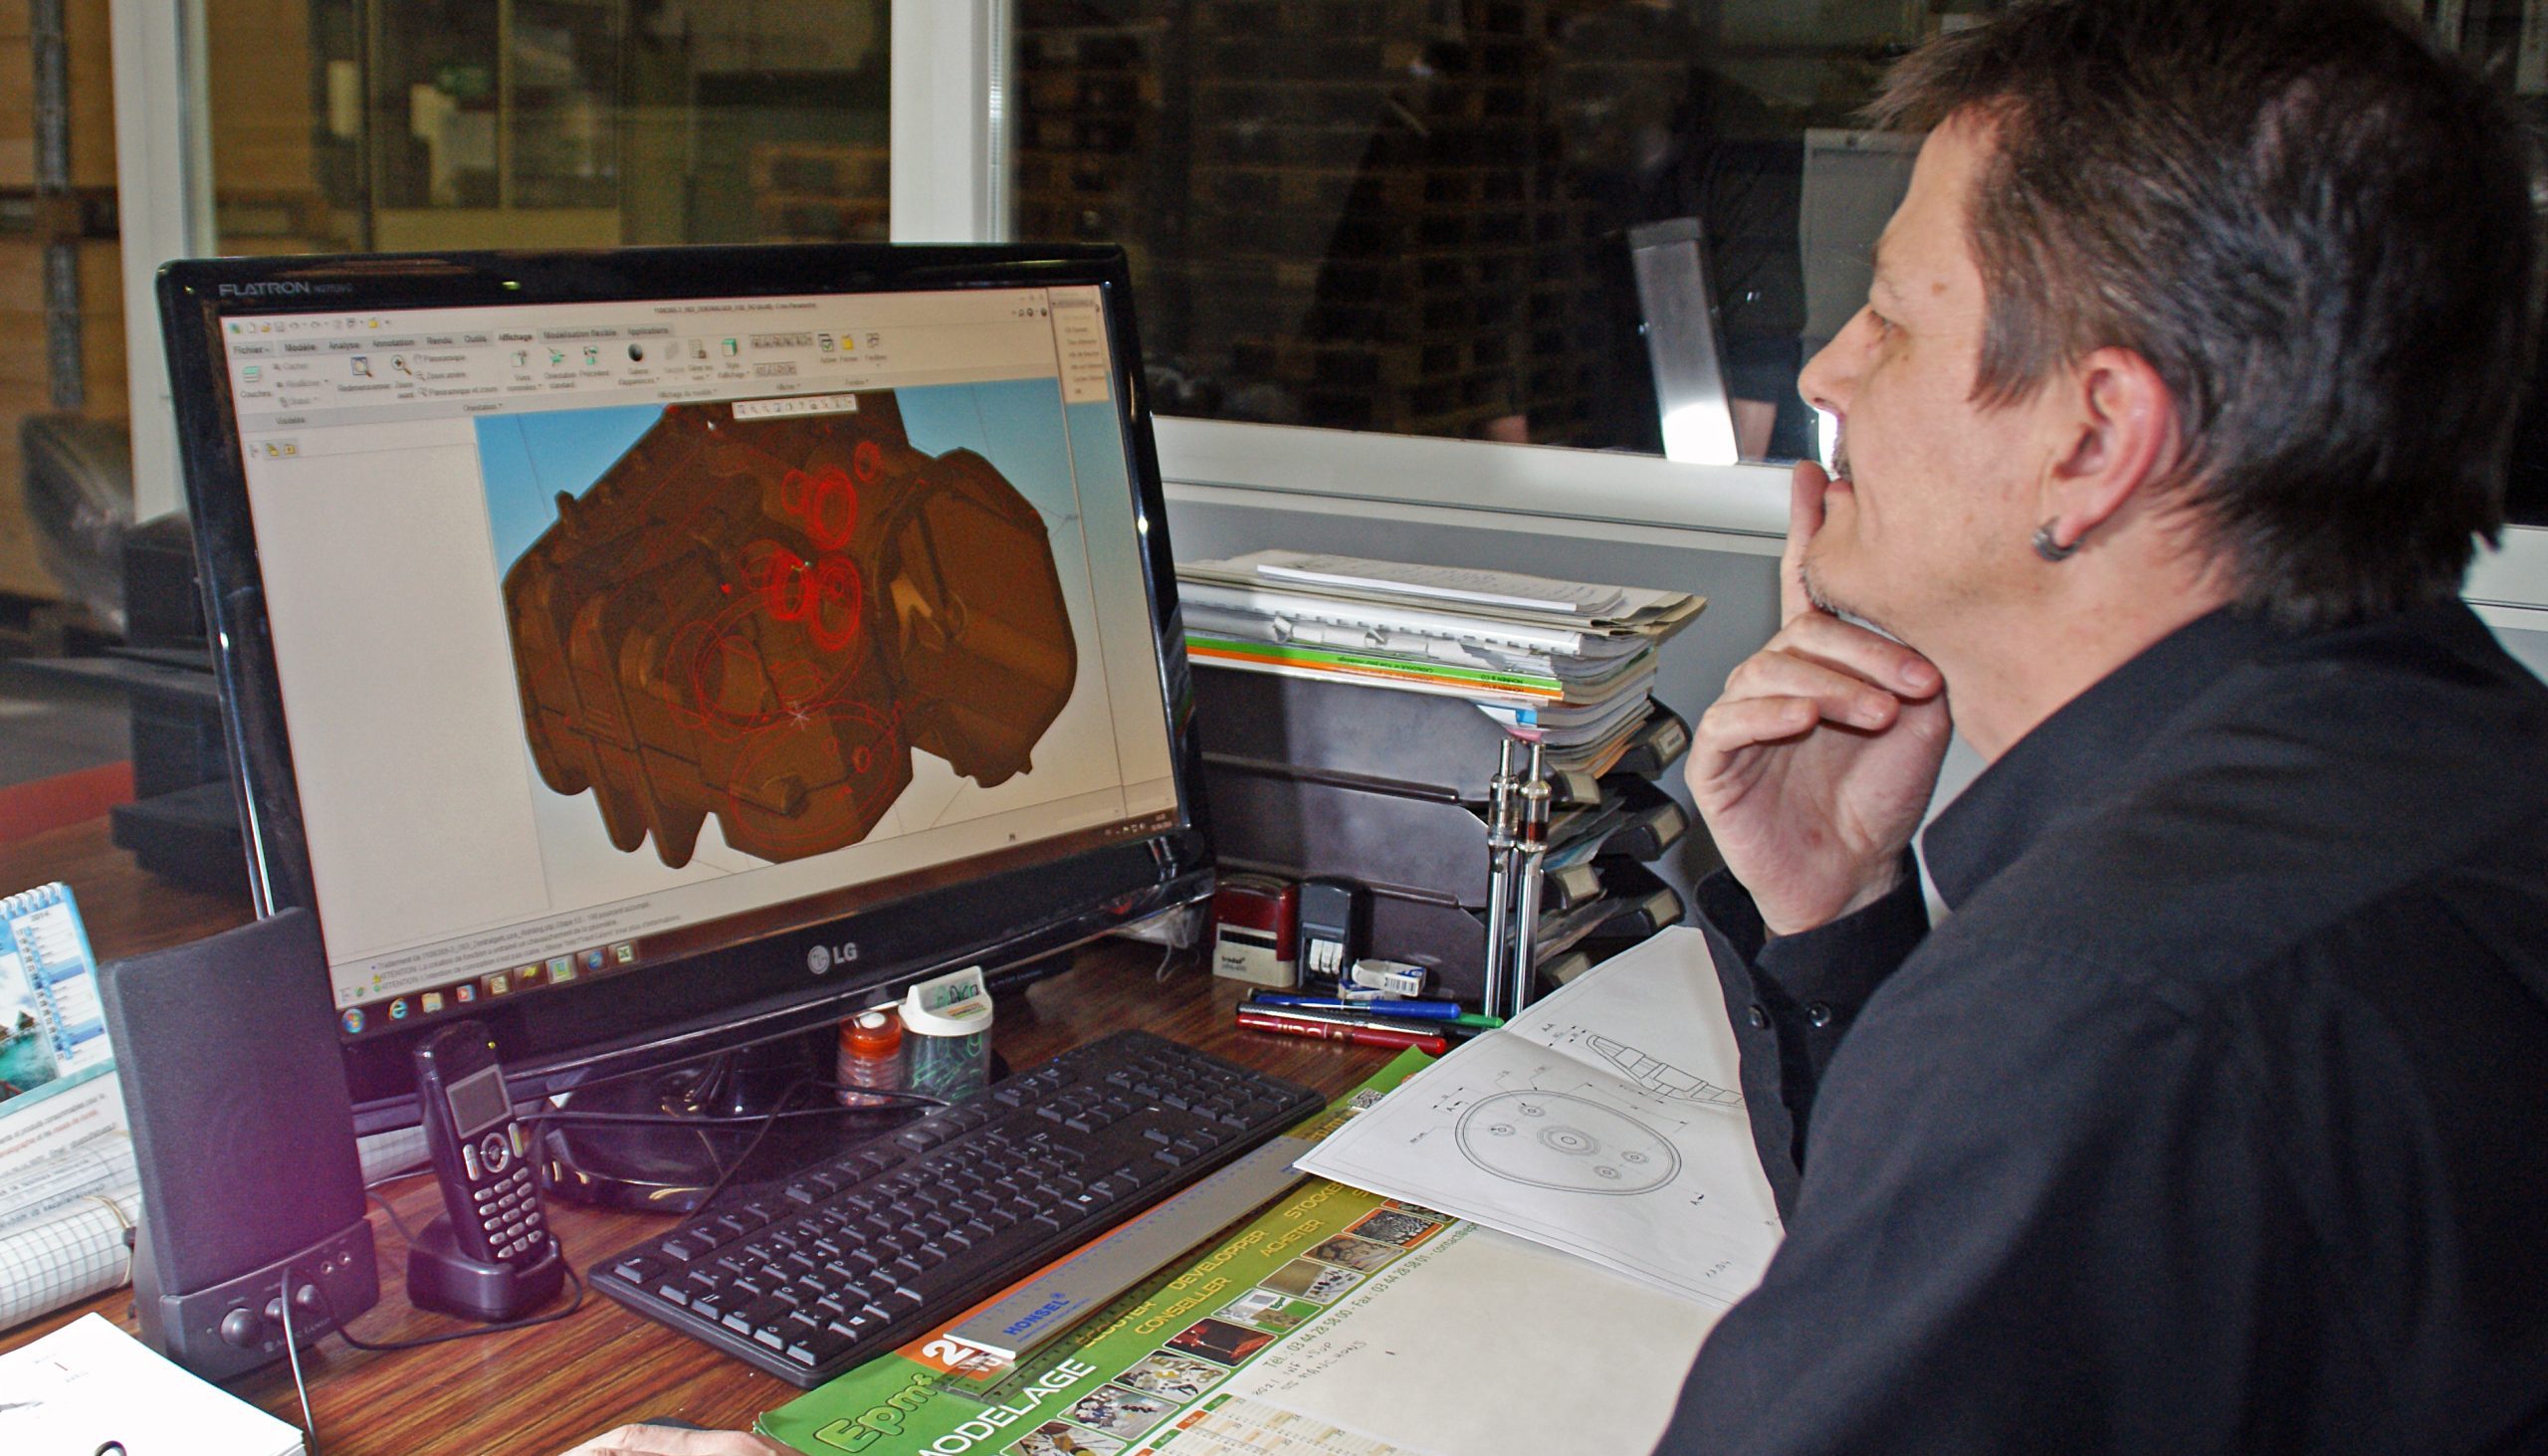
You provide us with a plan, an idea or an piece that already exists. Our technicians analyse the feasibility and design the complete tooling in-house, models, core boxes, core making, and this is carried out using SolidWorks. If the part can be optimised prior to production, we will point this out: geometry, material grade, wall thicknesses of the wall. Redesign to cost…